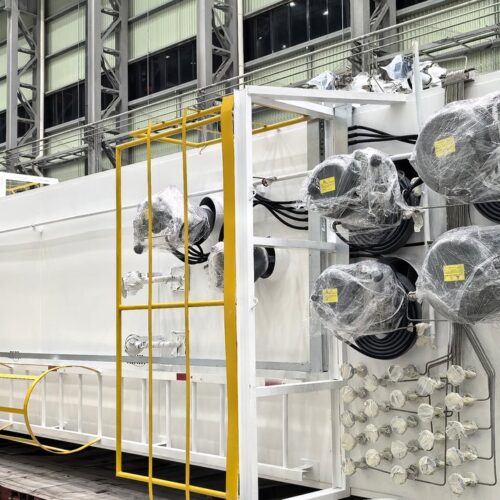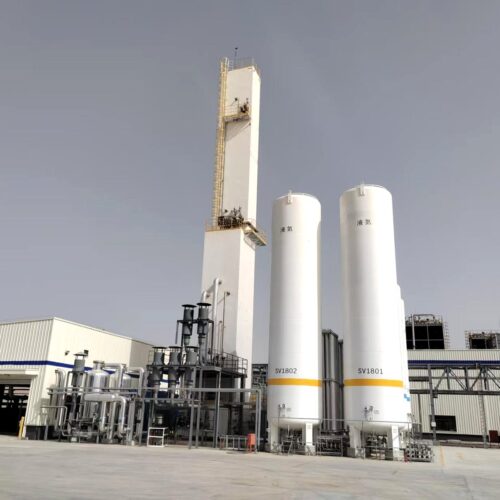
Cryogenic air separation plants for steel and metallurgy
Steel and non-ferrous metallurgy rely on cryogenic air separation for large-scale, high-purity industrial gases. We design and supply high-efficiency cryogenic ASU plants delivering oxygen at $\ge 99.6\%$ purity for blast furnace enrichment and smelting furnaces, high-purity nitrogen for protective atmospheres, and integrated rare gas recovery (argon, krypton, xenon) — along with plant retrofits and energy-saving upgrades.
Burner and lance duty reacts immediately to pressure fluctuations, so plant load control and oxygen network design determine whether steelmaking runs smoothly.
02
The right purity for the duty
Blast furnace enrichment and oxy-fuel combustion work well at 90–95%, while lancing, cutting and plant-wide networks operate at 99.6%. VPSA where low purity is acceptable cuts capital and power cost considerably.
03
Continuous operation with high availability
Steel production does not stop for maintenance windows, so liquid oxygen backup or a network of multiple plants covers planned and unplanned stops.
04
Existing plants worth upgrading
Many older air separation units consume well above current benchmark power. Replacing the compressor train, expander or column internals reduces consumption at a fraction of the cost of a new plant.
05
Argon for stainless and welding
Plants with stainless or welding demand often justify argon recovery as part of the oxygen plant.
TYPICAL REQUIREMENTS
Typical process requirements
Blast furnace oxygen enrichment
0.5 – 1.5 MPa(G)
Oxygen 90 – 99.6%
Basic oxygen furnace / converter
1.0 – 3.0 MPa(G)
Oxygen ≥99.6%
EAF burners and lances
0.8 – 2.0 MPa(G)
Oxygen ≥99.6%
Non-ferrous smelting (Cu, Pb, Zn)
0.5 – 1.5 MPa(G)
Oxygen, project specific
Annealing and protective atmosphere
0.3 – 1.0 MPa(G)
Nitrogen 99.999%
Stainless and welding
Battery limit
Argon ≥99.999%
RECOMMENDED CONFIGURATION
Recommended configuration
How we would configure the plant for this duty.
Cryogenic oxygen plant
For plant-wide networks and any duty requiring ≥99.6%, with optional nitrogen co-production and argon recovery from the same cold box.
ASU oxygen unit
For dedicated enrichment or combustion at 90–93% where capital and start-up time matter more than purity. Starts in minutes.
Liquid oxygen backup
Storage plus pump and vaporiser sized to cover the restart time, protecting the steelmaking line during unplanned stops.
Nitrogen plant
99.999% nitrogen for annealing and protective atmospheres, from the same cold box or as a dedicated cryogenic nitrogen plant.
Argon recovery
Crude and pure argon columns with de-oxidation and drying, delivering ≥99.999% argon for stainless steel and welding.
Retrofit and energy saving
Assessment of operating data, then targeted replacement of compressor, expander or column internals to cut specific power.
Often yes. We start from operating data and the original design, identify the losses and propose a targeted modification with an estimate of the achievable reduction in specific power.
Enough to cover the restart time of the air separation unit plus the acceptable interruption window of the steel process. One tonne of liquid oxygen equals roughly 700 Nm³ of gas.