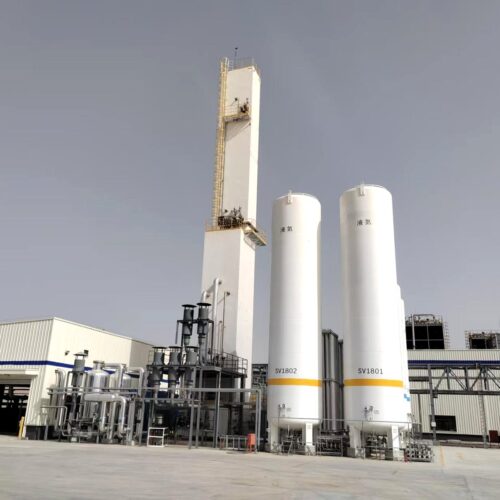
Air separation plants for chemical and coal chemical projects
Coal gasification, coal-to-chemicals, methanol, ammonia, ethylene oxide and refinery projects are the largest single consumers of industrial oxygen. We design and build cryogenic air separation units for these duties: oxygen at ≥99.6% and high flow, nitrogen for inerting and purging, argon recovery where justified, internal compression for high-pressure gasification and liquid oxygen backup.
Very large oxygen flows with a hard availability requirement
If the air separation unit stops, the gasifier or reformer stops with it, often with a costly and slow restart. Reliability engineering is part of the plant design.
02
Oxygen pressure matched to the gasifier
High-pressure gasification needs oxygen at several MPa, which points to internal compression: pumping a cryogenic liquid consumes far less power than compressing gas at ambient temperature.
03
Nitrogen for inerting, purging and transport
Most chemical projects also need nitrogen at moderate to high flow and 99.9–99.99% purity, from the same cold box.
04
Argon worth recovering
Above roughly 3,000 Nm³/h of oxygen, argon recovery usually pays back, and the site often has its own welding, stainless or specialty gas demand.
05
Energy as a headline figure
Oxygen is a major operating cost in a coal chemical complex, so guaranteed specific power in kWh per Nm³ is one of the most closely negotiated contract items.
TYPICAL REQUIREMENTS
Typical process requirements
Oxygen flow
Single or multiple trains, modular cold box
Several thousand Nm³/h upward
Oxygen purity
Column configuration and pressure profile
≥99.6%, sometimes ≥99.8%
Oxygen pressure
Internal compression usually preferred
Up to several MPa(G)
Nitrogen
Nitrogen column in the same cold box
99.9% – 99.99%, moderate to high flow
Argon
Crude and pure argon columns, de-oxidation
≥99.999% where recovered
Liquid products
Cryogenic tank, pump and vaporiser
LOX / LIN backup
Operating hours
Rotating equipment and sparing philosophy
≥8,000 h/y continuous
Control
Independent protection layer
DCS with interlock layer, SIL 2 or above
RECOMMENDED CONFIGURATION
Recommended configuration
How we would configure the plant for this duty.
Combined cold box
Oxygen, nitrogen and argon from one cold box sharing compression and refrigeration — the incremental cost of additional products is far lower than separate plants.
Internal compression
Cryogenic liquid pumped to pressure and re-gasified in the main heat exchanger, giving lower specific power at high pressure and flow.
Liquid oxygen backup
Storage and vaporisation sized to the time needed to restart the plant or protect the process unit during a planned shutdown.
Argon recovery
Crude argon column coupled to the main column, de-oxidation, drying and pure argon distillation to ≥99.999%.
Robust control and safety
DCS with engineer, operator and historical stations plus an independent interlock layer for liquid oxygen level, hydrocarbon, surge and overspeed.
Modular shipment
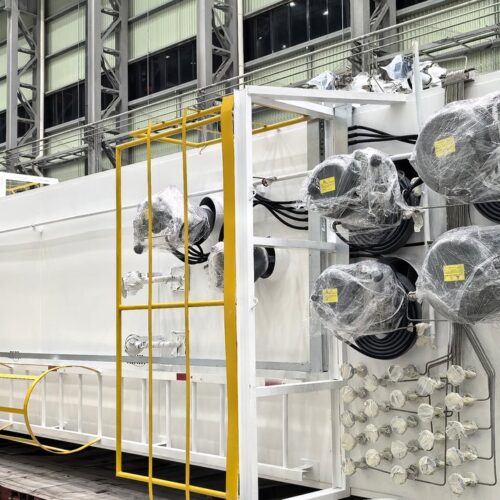
Cold box assembled and function-tested in our workshop, then shipped as a modular unit to reduce site welding and construction time.
Yes. The guarantee is stated in kWh per Nm³ of product at defined ambient temperature, load and product pressure, and verified at the performance test.
Liquid oxygen and nitrogen storage with automatic vaporisation keeps critical consumers supplied while the plant restarts. Storage size is agreed with the customer.
Yes. Equipment and supervision, turnkey EPC with one point of responsibility, or build-own-operate with long-term gas supply.
START WITH YOUR PROCESS
Send us your oxygen balance.
Oxygen and nitrogen flow, purity, discharge pressure, argon requirement, liquid backup and site conditions are enough to begin — preliminary configuration within 24 hours.